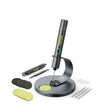
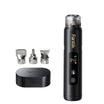
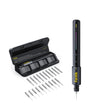
When setting up a soldering iron for heat-set inserts, start with a material-specific temperature rather than the tool's maximum setpoint: roughly 437°F (225°C) for PLA, 473°F (245°C) for PETG, and 509°F (265°C) for ABS/ASA. These figures are practical starting points rather than rigid technical standards, and using the right tip profile matters just as much as dialed temperature.
From that baseline, alignment, contact time, and a controlled press determine whether the brass insert seats perfectly flush or damages the surrounding plastic.
What Temperature Should You Start With for PLA, PETG, and ABS/ASA?
The table below outlines practical starting points for common filaments. Treat each value as an initial baseline, then adjust based on how the plastic softens and flows around the brass.
| Filament | Starting point | What to watch | Evidence status |
|---|---|---|---|
| PLA | ~437°F / 225°C | Rapid softening; insert can sink too fast | Practical starting point, not a standard |
| PETG | ~473°F / 245°C | Stringing or a glossy melt ring around the boss | Practical starting point, not a standard |
| ABS/ASA | ~509°F / 265°C | Slower melt; watch for fumes or discoloration | Practical starting point, not a standard |
These numbers start slightly above each polymer's typical print temperature, because distinct filament thermal behaviors require more heat than baseline print profiles suggest. They are practical workshop guidelines rather than strict manufacturer specifications or safety thresholds.
Why the Table Is Only a Starting Point
Filament blends vary across brands, and additives such as glass fiber or color pigments alter how quickly polymers soften under heat. Insert size and the contact surface area of your tip also shift thermal delivery, which means the exact same displayed setpoint can behave differently across distinct parts.

Keep four factors distinct: maximum tool temperature, chosen working setpoint, tip thermal capacity, and thermal recovery speed under load. A high maximum temperature rating does not guarantee rapid or consistent heat transfer into a brass insert.
How Temperature, Insert Size, and Printed Geometry Change Heat Delivery
A larger brass insert pulls heat out of an iron tip faster than a smaller insert, requiring steady contact rather than an aggressive temperature increase. Meanwhile, thin walls and compact printed bosses tolerate very little radiant heat or excess force before deforming beyond the insert profile.
Why Larger Inserts Change the Heat Balance
A larger insert carries greater thermal mass, demanding more thermal energy to bring its entire body to the plastic's softening point. When a tip makes contact with only a small portion of the insert rim, heat conducts slowly, risking local plastic melt before the core is hot enough to sink smoothly. This is a contact area and thermal recovery issue, not a need for maximum iron temperature.
What to Adjust When the Result Changes
- Tip fit and contact area first. Confirm that the tip seats firmly and squarely against the insert rim rather than perching off-center.
- Alignment and pressure second. Maintain light, axial downward force to guide the insert straight into the printed hole.
- Contact time third. Holding contact for an extra second or two often resolves slow seating more effectively than turning up the heat.
- Setpoint only after the above are controlled. Make small, incremental temperature adjustments only after verifying mechanical contact and alignment.
Which Tip Profile Should You Use for Heat-Set Inserts?
Use a dedicated insert tip whenever its centering pilot matches the internal bore and its shoulder bears directly on the insert rim. A general-purpose soldering tip can work only if it holds the insert square without touching or melting the printed boss.
When a Dedicated Insert Tip Is the Better Choice
- A dedicated pilot pin fits inside the insert bore, preventing the insert from tilting off-axis during installation.
- A flat shoulder bears evenly on the rim of the insert rather than contacting the adjacent plastic wall.
- Greater contact surface area delivers heat evenly into the brass core, which is especially helpful for larger threads.
If the tip pilot does not match your insert bore size, these alignment benefits disappear, and forcing mismatched geometry will produce a crooked joint.
When a General Soldering Tip May Be Workable
A standard conical or chisel tip can seat an insert if you can steady it squarely against the top face without letting the shoulder drag against the plastic boss. This technique demands precise manual control, as any slip risks scarring the surrounding print. Do not assume general electronics tips provide correct centering geometry; verify physical fit against your brass fastener before attempting an assembly.

How to Install a Brass Insert Flush Without Over-Melting
Work on a stable, heat-resistant surface and treat both the iron tip and the brass insert as hot throughout the process. Keep hands and clearing tools away from the heated tip, and follow this sequential technique:
- Prepare the part and insert. Inspect the printed hole to ensure it is clean of debris and matches the insert specification.
- Seat the insert on the tip. Position the insert squarely against the heated tip so the brass absorbs thermal energy before contacting the plastic.
- Align the iron square to the hole. Hold the iron perpendicular to the boss surface so the fastener drives straight down.
- Heat and press gradually. Allow the hot brass to soften the plastic using gentle, steady pressure rather than pushing aggressively.
- Stop just short of flush. Relieve pressure just before reaching full depth to avoid plunging the insert below the surface.
- Finish with a straight, controlled push. Level the insert rim with a light, square movement so it sits flush with the boss face.
- Check flushness and tilt. Check the part from the side immediately; make minor adjustments while the surrounding plastic remains pliable.
- Hold and let it stabilize. Keep the assembly steady while the plastic solidifies around the knurling before handling or fastening.
Stop heating immediately if the plastic discolors, smokes unusually, or bulges outside the boss diameter. If overheating occurs, reduce the setpoint or contact time before attempting the next installation.
How to Fix Crooked, Loose, or Over-Melted Inserts
Identify the symptom and apply the single primary correction before adjusting other parameters. Once the insert cools, managing torque limits for plastic fasteners prevents stripping the new brass threads during assembly.
If the Insert Is Crooked or Recessed
- Crooked insert: verify perpendicular alignment before pressing; correct the tool angle instead of applying heavier off-axis force.
- Recessed below surface: stop pressing earlier and decrease contact dwell time slightly.
- Melted ring around the boss: shorten contact dwell time and ensure the tip shoulder does not touch the outer plastic.
If the Insert Spins, Loosens, or Heats Unevenly
- Spins under torque: inspect whether the printed hole diameter is oversized for the insert knurling before adjusting heat.
- Weak pull-out retention: check printed wall thickness around the boss to verify sufficient polymer volume for knurl engagement.
- Inconsistent heat transfer: clean oxidation off the tip face and check surface contact against the insert rim before raising temperatures.
FAQs
How should I choose a starting temperature for a filament that's not PLA, PETG, or ABS/ASA?
Do not borrow temperature values from a different polymer family. Check the filament manufacturer's documented print-temperature range and use the lower half of that printing bracket as a baseline starting point. Test on a printed scrap piece first, observing how cleanly the plastic yields without scorching before running inserts into final parts.
Why is molten plastic pushing up into the internal threads?
Plastic enters internal threads when an insert is driven too deeply or when the tip diameter is smaller than the insert bore, allowing liquefied plastic to displace upward into the hollow center. Use a tip with an integrated pilot pin that seals the inner opening, and stop pressing the instant the insert rim sits flush with the printed surface.
Can an insert be adjusted or removed after the plastic cools?
Once the plastic solidifies, an insert cannot be moved without reheating. If an insert seated crooked, reheat it gently with your soldering iron tip under minimal axial pressure until the plastic softens, realign it square to the boss, and allow it to cool completely before applying mechanical load.


Leave a comment
This site is protected by hCaptcha and the hCaptcha Privacy Policy and Terms of Service apply.